Note: This article synthesizes information from reputable engineering, machining, industrial heating, bearing, manufacturing, and safety resources. Source links are intentionally omitted from the publishable copy as requested.
There is something deeply satisfying about a workshop technique that appears to violate common sense. Take two metal parts that do not fit together. Heat one of them without melting it, slip the pieces together, wait a little while, and suddenly they are locked in an embrace so tight that a hydraulic press might start reconsidering its career choices.
That is the basic magic of shrink-fitting, although the actual explanation involves thermal expansion rather than sorcery. In machine shops, industrial maintenance, bearing installation, and precision toolholding, the technique has been used for years to create strong interference fits. Commercial induction shrink-fit systems make the process fast and repeatable, but they can also be expensive. That naturally raises the favorite question of every ambitious home shop owner: How complicated could it really be?
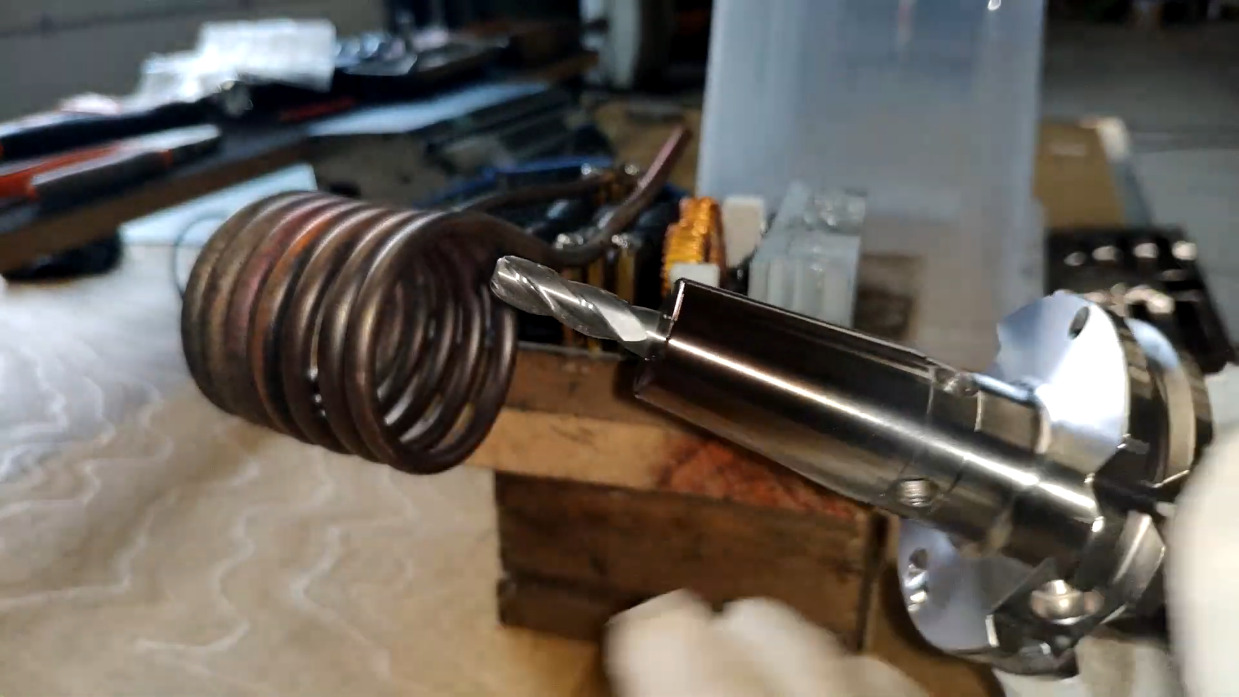
One particularly elegant homebrew answer uses a relatively simple induction heater built around a high-current power supply, a zero-voltage-switching driver, and a heavy copper work coil. The setup demonstrates how a modest collection of electronics can turn electromagnetic induction into a remarkably effective machine-shop tool.
What Is Shrink-Fitting, and Why Does It Work?
A shrink fit is a type of interference fit. At normal temperature, the outer component has an opening that is slightly smaller than the mating part. Trying to force the two together mechanically can require enormous pressure and may damage the surfaces. Instead, the outer part is heated so that it expands temporarily.
The dimensional change may be small enough to escape the naked eye, but machining lives in a world where a few thousandths of an inch can separate “perfect fit” from “where did the hammer go?” Once the bore expands sufficiently, the mating shaft, cutter, bushing, bearing, or other component can slide into place. As the heated part cools, it contracts and develops a powerful clamping force.
Thermal expansion does the heavy lifting
Metals generally expand when heated and contract when cooled. The approximate change in dimension depends on the original size of the part, the temperature change, and the material’s coefficient of thermal expansion. In simplified form, the relationship can be expressed as:
Change in size = original dimension × thermal expansion coefficient × temperature change
That equation explains why accurate dimensions matter so much. A homebrew shrink-fit operation is not simply a contest to see how orange the steel can become. The interference, material, wall thickness, geometry, and target temperature all influence whether the part slips together beautifully or becomes an expensive lesson in metallurgy.
The Homebrew Induction Heater Approach
The maker project that inspired this discussion takes a wonderfully direct route. Its basic system uses a 48-volt, 20-amp power supply, an off-the-shelf ZVS induction heater driver, and a substantial copper coil surrounding the workpiece. Nominally, that power supply represents nearly a kilowatt of electrical capability, which is plenty of energy to demand respect even before the metal starts getting hot.
The workpiecein this case a steel tool holderis placed within the coil. When the induction circuit is energized, alternating current in the coil produces a rapidly changing magnetic field. That field induces electrical currents inside the conductive metal. Resistance to those currents generates heat within the workpiece itself. Ferromagnetic materials can also experience additional magnetic losses, depending on the material and operating conditions.
This is the key advantage of induction heating: the copper coil does not have to become a glowing heating element and slowly transfer its heat into the holder. The electromagnetic field causes the workpiece to generate heat directly.
Why a ZVS driver is useful
Zero-voltage-switching circuits are popular in DIY induction heaters because they can drive a resonant circuit efficiently at high frequency. Rather than brutally switching power under the worst possible electrical conditions, a resonant ZVS topology is designed so switching occurs under conditions that reduce switching losses and stress.
That does not make an inexpensive ZVS board indestructible. Current can be substantial, component cooling matters, coil geometry changes the electrical load, and a poorly matched setup can turn semiconductor components into tiny commemorative smoke machines. Still, packaged ZVS modules have made experimental induction heating much more accessible than it once was.
From Undersized Bore to Nearly Zero Runout
For shrink-fitting a cutting tool, the holder begins with a precisely machined bore that is slightly smaller than the tool shank. Both mating surfaces need to be exceptionally clean. Dirt, oil residue, chips, burrs, corrosion, and dimensional mistakes do not become less troublesome merely because electricity is involved.
In the featured homebrew setup, the steel holder is heated rapidly in the induction coil to roughly 250 to 300 degrees Celsius. The bore expands enough for the tool to be inserted. As the holder cools, the bore contracts around the shank.
The attraction for machining is obvious. A properly manufactured shrink-fit holder can provide excellent concentricity, strong gripping force, a slim profile, and no collet nut protruding around the cutting tool. That can be especially useful for high-speed machining or applications where clearance around the cutter matters.
Commercial shrink-fit tooling systems are engineered around these advantages. They commonly pair dedicated holders with controlled induction heating cycles and purpose-designed coils. The homebrew version strips the concept down to its essentials and proves that the underlying physics does not care whether the machine has a glossy touchscreen or a plywood shelf nearby.
Why Induction Heating Is So Well Suited to Shrink-Fitting
Fast, localized heating
An oven heats the part, the air, the racks, and eventually a noticeable portion of the room. A torch can heat quickly, but uniformity depends heavily on technique. Induction heating can concentrate energy in the region placed within the work coil, allowing the outer component to expand before too much heat migrates into the inner component.
That temperature difference is valuable. If both the holder and tool heat at the same rate, both expand, and the clearance you were hoping to create can vanish like a 10 mm socket.
Repeatability
Industrial induction systems are popular partly because power, time, coil position, and temperature can be controlled. Once a process is developed for a particular part, it can be repeated with far less variation than a purely manual heating method.
A basic DIY machine will not automatically provide industrial process control, but it can borrow the same philosophy. A fixed holder position, consistent coil geometry, reliable timing, and genuine temperature measurement are far better than simply heating until the operator feels spiritually confident.
No open flame
Induction heating avoids the direct flame of a torch. That can reduce localized scorching and makes controlled heating easier in many applications. It does not, however, make the operation harmless. The workpiece can still cause severe burns, and the electrical system itself may involve dangerous current, exposed conductors, hot components, and stored energy.
The Copper Coil Is More Important Than It Looks
The work coil is not merely a decorative spiral of copper. Its diameter, number of turns, spacing, position, and distance from the workpiece influence coupling and heating behavior. Industrial induction systems often use coils designed specifically for the geometry of the component.
For a cylindrical tool holder, a helical coil surrounding the area to be expanded is an intuitive solution. The goal is to heat the relevant section quickly and reasonably uniformly. Too large a gap can reduce coupling. Poor alignment may produce uneven heating. A coil positioned over unnecessary areas wastes energy and may heat parts of the holder that would be better left cooler.
High-power or repeated operation can also create significant heat in the work coil and resonant components. Industrial machines frequently use liquid-cooled coils. A small experimental system may survive short cycles without elaborate cooling, but duty cycle remains important. “It worked once” is not the same engineering specification as “it can repeat this operation fifty times before lunch.”
Temperature Control Matters More Than Dramatic Metal Colors
One of the biggest traps in homebrew heat processing is assuming that visible color is a precision thermometer. Surface oxidation, lighting, alloy composition, viewing conditions, previous heat treatment, and surface finish can all affect appearance.
A better setup uses an appropriate temperature-measurement method and establishes a controlled heating cycle for the exact holder and material involved. Infrared thermometers can be useful, but emissivity and reflective surfaces may affect readings. Contact sensors have their own practical limitations during rapid induction heating. The important point is that temperature measurement is an engineering problem, not an optional decoration.
Overheating a precision tool holder can alter its properties, increase oxidation, distort the geometry, or shorten its service life. Commercial systems justify part of their cost through process control, coil design, cooling, safety features, and repeatabilitynot because manufacturers discovered a secret variety of expensive electricity.
Homebrew Shrink-Fitting Is About Precision, Not Brute Force
The interference between the two components must be designed correctly before the heater is switched on. Too little interference may produce inadequate holding force. Too much can require excessive temperature, generate extreme stresses, prevent assembly, or damage one of the parts.
A useful workflow begins with measurement and calculation. Confirm the actual bore diameter, tool shank diameter, roundness, surface condition, materials, and required thermal expansion. For an experimental shop fixture, test pieces are far cheaper than sacrificing a premium cutter and holder on the first attempt.
Assembly also needs to happen quickly. The moment the heated holder meets a cooler tool, heat begins transferring between them. Clearance can disappear rapidly. The tool should therefore be aligned and ready before heating begins. Stops, depth-setting fixtures, and safe handling tools can make the process far more predictable.
Shrink-Fitting Is Not Limited to Cutting Tools
The same principle appears throughout mechanical engineering. Bearings can be heated to simplify mounting onto shafts. Gears, sleeves, couplings, bushings, motor components, and other assemblies can use controlled thermal expansion to create or release interference fits.
Induction heating is particularly attractive when only one region needs to be heated. Industrial examples include heating a gear bore before shaft installation, expanding bearing rings, fitting sleeves, and assembling components that would otherwise require large mechanical presses.
Reheating can sometimes reverse the operation. If the outer component expands faster than the inner part, a previously locked assembly may be separated. This is why induction heaters are also popular for maintenance jobs such as loosening stubborn metal components. The exact procedure, however, must respect the materials and heat treatment of the parts involved.
Safety: The Part That Should Never Be Homebrewed Away
A compact induction heater may look friendlier than a gas torch, but it combines several hazards in one enthusiastic little package. The power supply can deliver substantial current. The switching circuit can contain high-frequency electrical energy. Conductive objects near the coil may heat unexpectedly. The workpiece may remain dangerously hot long after the power is switched off.
A sensible build should use properly rated wiring, secure terminals, fusing or other suitable overcurrent protection, insulated and enclosed electronics, a dependable means of disconnecting power, and physical arrangements that keep hands away from energized components. Exposed jewelry and loose metal objects have no business wandering near a working high-current induction system.
Hot-part handling deserves equal attention. Use appropriate tools and heat-resistant personal protective equipment. Create a clearly defined cooling area. Do not place a freshly heated holder on a bench next to ordinary cold parts unless your workshop enjoys practical jokes with consequences.
Anyone without the knowledge to design and troubleshoot high-current power electronics safely should treat a DIY induction heater as an advanced project rather than a beginner’s shortcut. Buying a proven system is considerably cheaper than repairing a fire-damaged shop.
What Makes This Simple Induction Heater So Appealing?
The charm of the project is not that it replaces every commercial shrink-fit machine. It does not. A production shop running expensive tooling all day needs repeatability, controlled heating, cooling, ergonomic fixtures, and safeguards that a simple bench prototype may not provide.
What the project does exceptionally well is reveal how accessible the core technology has become. A robust power supply, a resonant induction driver, and a correctly arranged copper coil can create enough controlled heat to perform a genuinely useful machining operation.
It is also a beautiful example of technologies crossing workshop boundaries. The same basic induction-heating principles appear in heat treatment, bearing installation, brazing, forging, manufacturing, and even kitchen appliances. In the home shop, those principles can become a practical tool for solving problems that once demanded a torch, oven, or large press.
Experience Notes: What a First Homebrew Shrink-Fitting Session Usually Teaches
Workshop experience with homebrew induction heating tends to begin with an immediate realization: the heating happens faster than expected. A person familiar with ovens or even propane torches may mentally prepare for a leisurely warm-up. Then the induction system is energized, the temperature starts climbing, and the entire workflow suddenly feels as though someone pressed the fast-forward button.
That speed changes everything. Before starting a heating cycle, the mating tool needs to be clean, measured, oriented, and positioned within easy reach. The depth stop or fixture needs to be ready. Heat-resistant handling tools need to be in the correct place rather than hiding beneath a collection of clamps. A successful shrink fit often feels almost boring because the preparation was good: heat, insert, verify position, cool. A poorly prepared attempt can become an awkward race against thermal contraction.
Another common lesson is that coil position matters more than beginners expect. Moving the workpiece slightly can change where heat is concentrated. A holder with a thick section may respond differently from a slender one even when the bore diameter is similar. The machine may be electrically simple, but the heating process still rewards consistency. Marking a repeatable workpiece position or building a nonconductive support fixture can transform an improvised experiment into a far more predictable tool.
Cleaning also becomes an obsession surprisingly quickly. A tiny burr that seemed harmless at room temperature can ruin the brief assembly window. Oil can smoke. Chips can interfere with seating. Oxidation and residue can affect the fit. The best experience usually comes from treating the operation like precision assembly rather than blacksmithing with extra capacitors.
Then there is the temptation to overheat. The first instinct is often, “A little hotter will give me more time.” Sometimes it does. It can also oxidize the holder, change material properties, stress components, and turn a controlled fitting process into a metallurgical guessing game. Experienced practice moves in the opposite direction: determine the minimum reliable heat needed to achieve the required expansion, then make the cycle repeatable.
Cooling introduces another practical lesson. The assembly may look finished while still being far too hot to measure accurately or place into service. Dimensions continue changing as the temperature equalizes. For precision machining, the tool should be allowed to return to a stable temperature before final runout checks or critical length measurements.
The most rewarding moment is usually the first successful fit. The tool slips into a bore that rejected it seconds earlier, and then the holder cools into a solid, concentric assembly with no collet nut and no tightening wrench. It feels almost too easy, which is precisely why the preparation and safety discipline matter. The operation itself may take seconds; getting those seconds right is the real craft.
Finally, the experience tends to change how a maker looks at induction heating in general. What began as a specialized solution for shrink-fitting starts suggesting other controlled-heating jobs: freeing suitable seized components, heating rings and sleeves, experimenting with thermal assembly, or developing purpose-built fixtures. The important lesson is not that an induction heater should be pointed at every stubborn piece of metal. It is that localized, rapid, non-contact heating is an extraordinarily useful capability when paired with measurement, restraint, and an understanding of the materials involved.
Conclusion
The simple induction heater for homebrew shrink-fitting is a perfect example of a workshop project that looks deceptively modest while demonstrating serious engineering. A high-current supply, ZVS driver, and copper coil can turn electromagnetic induction into rapid, localized heating capable of temporarily expanding a precision metal holder.
The real achievement is not merely making steel hot. The interesting part is controlling heat well enough to exploit thermal expansion without sacrificing accuracy or damaging the components. Successful shrink-fitting depends on correct interference, clean surfaces, suitable materials, consistent heating, fast assembly, controlled cooling, and respect for electrical and thermal hazards.
Commercial shrink-fit machines remain the right choice for demanding production environments. For skilled experimenters and home machinists, however, a carefully designed induction heater offers a fascinating route into precision thermal assemblyand a reminder that sometimes the smartest way to make two parts fit is to convince one of them to become temporarily larger.